1. Cylinder Making (Gravure Plate Engraving)
The customer’s design is engraved onto a gravure cylinder using laser or mechanical engraving. The cylinder surface is etched with tiny cells that hold ink, ensuring high-resolution, repeatable printing.
2. Printing
The engraved cylinder is mounted on a gravure printing press. Ink is transferred from the cylinder onto the OPP or PP film substrate through multiple color stations. This step builds the design layer by layer, achieving vivid colors and sharp details.
3. Drying
After each ink layer is printed, the film passes through a heated drying tunnel. Hot air evaporates solvents and cures the ink, preventing smudging and ensuring good adhesion. Complete drying is essential before the lamination step.
4. Lamination (Composite Bonding)
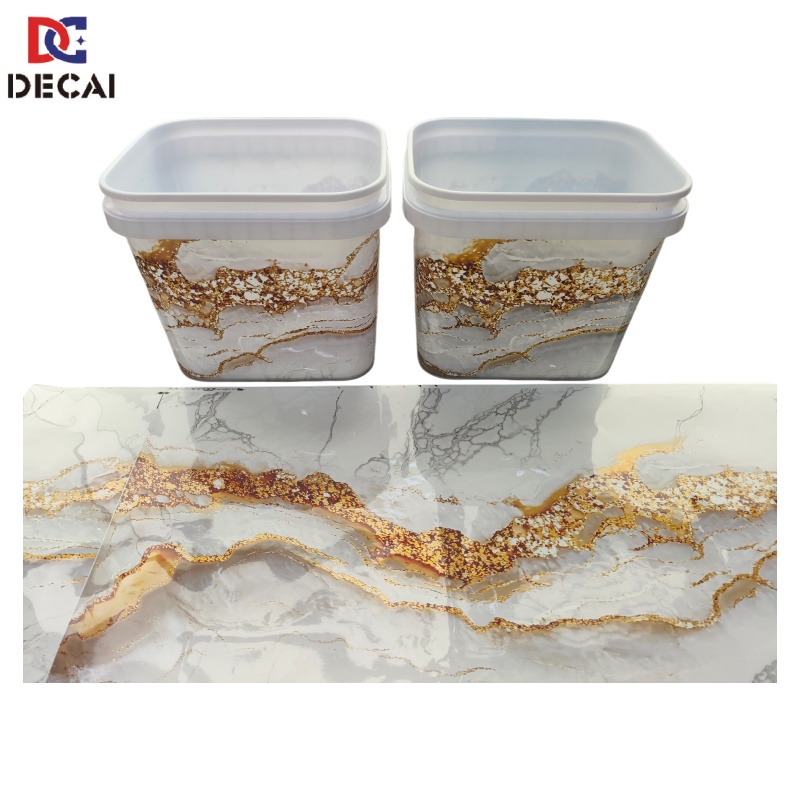
Once the printed film is fully dried, it is laminated with a secondary backing layer (typically a white or opaque PP film) using an adhesive or thermal bonding process. This composite structure provides opacity, stiffness, and improved handling during injection molding. The lamination is carried out under controlled temperature and pressure to achieve a strong, bubble-free bond.
5. Slitting / Die-Cutting
The laminated master roll is then slit into narrower rolls or die-cut into individual label shapes according to customer requirements. Precision cutting ensures clean edges and accurate dimensions for reliable placement in molds.
6. Quality Inspection
Each finished roll or batch undergoes thorough inspection. Key checks include color accuracy, print clarity, lamination integrity (no bubbles or delamination), dimensional accuracy, and adhesion strength. Defective material is rejected.
7. Packaging
Inspected rolls are wrapped in protective film to prevent dust and moisture damage, then packed into sturdy cartons with clear labeling for size, design, and batch number.
8. Shipping
Packaged goods are palletized, shrink-wrapped, and dispatched with the necessary shipping documents for timely delivery.
Post time: Oct-23-2026